








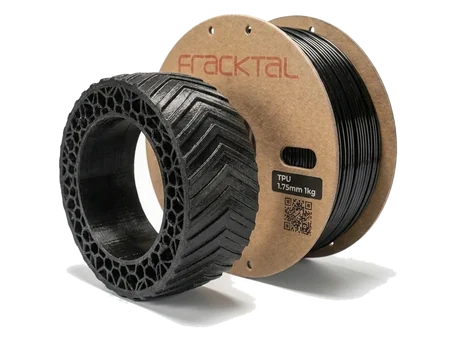



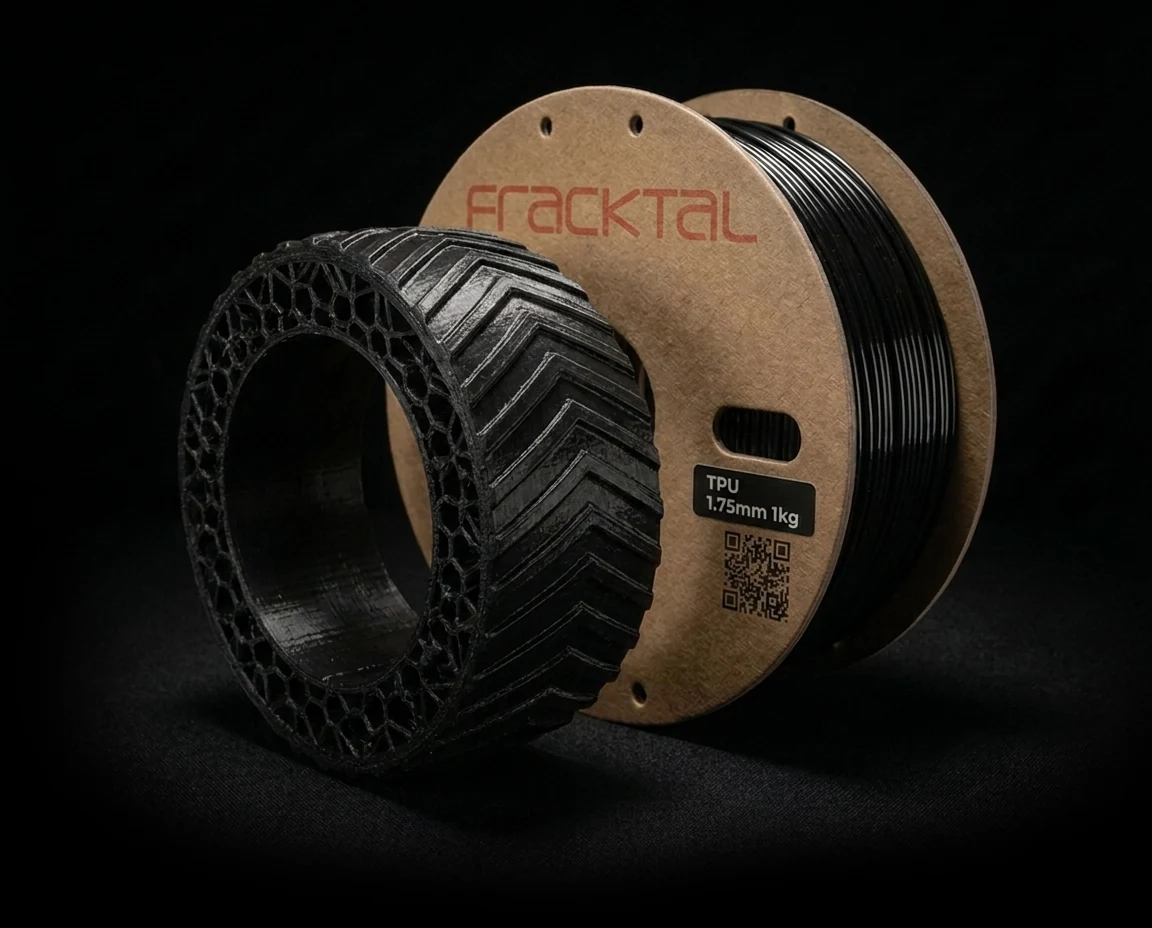
TPU 95A
Flexible Filament
A Shore 95A polyurethane: flexible, tear-resistant and hard to wear out. Seals, gaskets and protective housings.
Quick Reference
- Material properties
- Flexible / Elastomeric
- Thermoplastic Polyurethane (TPU)
- None
- 28 MPa
- 60 °C
- 1.21 g/cm³
- Moderate — dry 60 °C / 8 h before printing
- 225–235 °C
- ≥ 0.4 mm
- Brass
- 30–50 °C
- Not required
- Sand, trim with knife; solvent bonding possible
Material Property Profile
Values scored 0–10 from measured mechanical data and print process behaviour. Select a material above to compare properties.
Key Properties
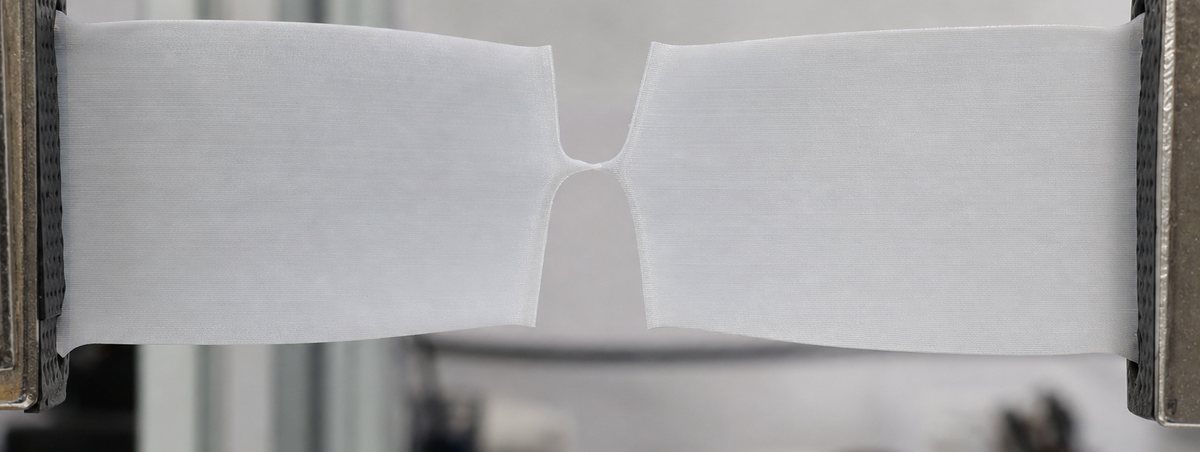
Judge TPU on hardness, elongation and tear. Tensile strength is the wrong question to ask a seal.

Machine Requirements
The extruder decides. A direct drive prints TPU; a Bowden fights it the whole way.
| Requirement | Minimum Spec | Recommended |
|---|---|---|
| Nozzle Temperature | 220 °C | 225–235 °C |
| Bed Temperature | 30 °C | 40–50 °C |
| Enclosure | Open | Not required |
| Extruder | Direct drive | Direct drive (Bowden not recommended) |
| Nozzle Material | Brass | Brass 0.4–0.6 mm |
| Cooling Fan | 25 % | 50–75 % |
Direct drive extruder required. TPU 95A is too soft and flexible for Bowden tubes. The filament buckles and jams in the gap between tube and nozzle. Disable or minimise retraction (≤ 1 mm, ≤ 25 mm/s) to prevent buckling inside the drive gear. TPU holds well on texture and poorly on smooth glass — the eight causes of a print that will not stick.
Applications by Industry
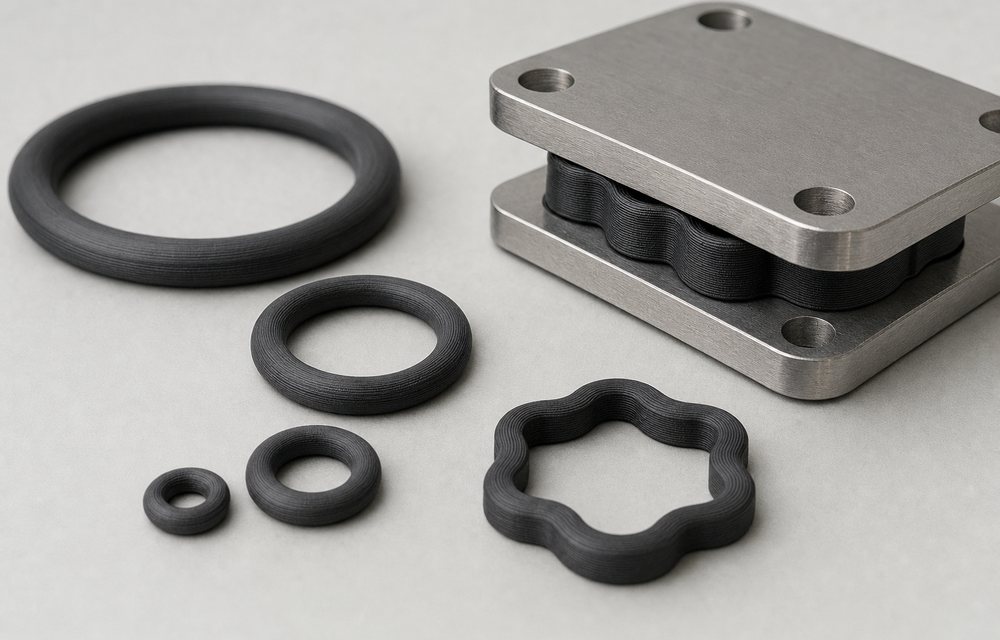
Seals & Gaskets
- Custom O-rings & seals
- Compression gaskets
- Weatherstrip profiles
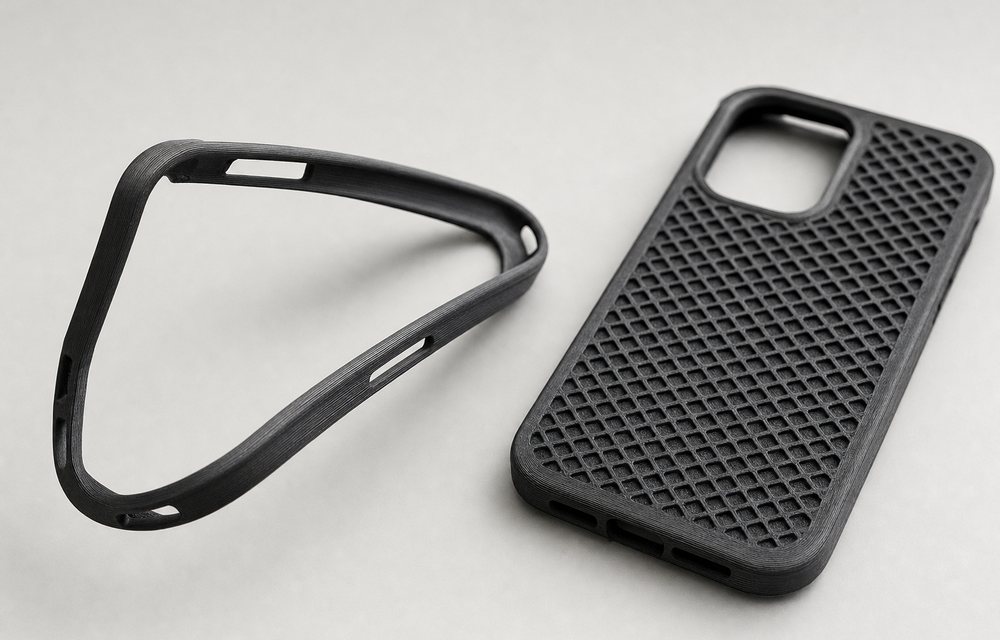
Consumer / Protective
- Phone cases & bumpers
- Grip covers
- Wearable straps
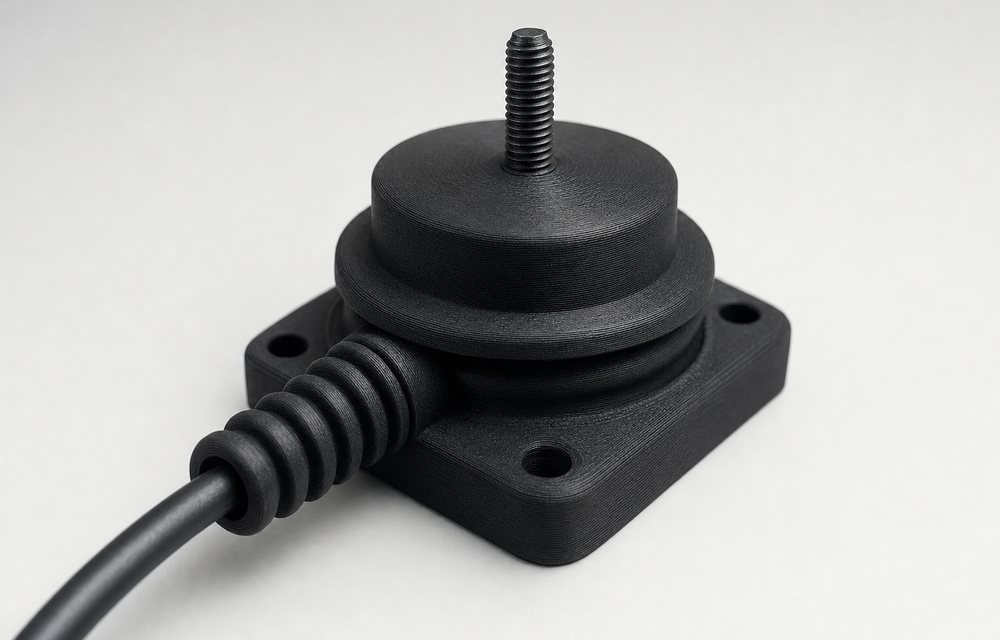
Industrial
- Vibration dampening mounts
- Flexible hose connectors
- Cable strain reliefs
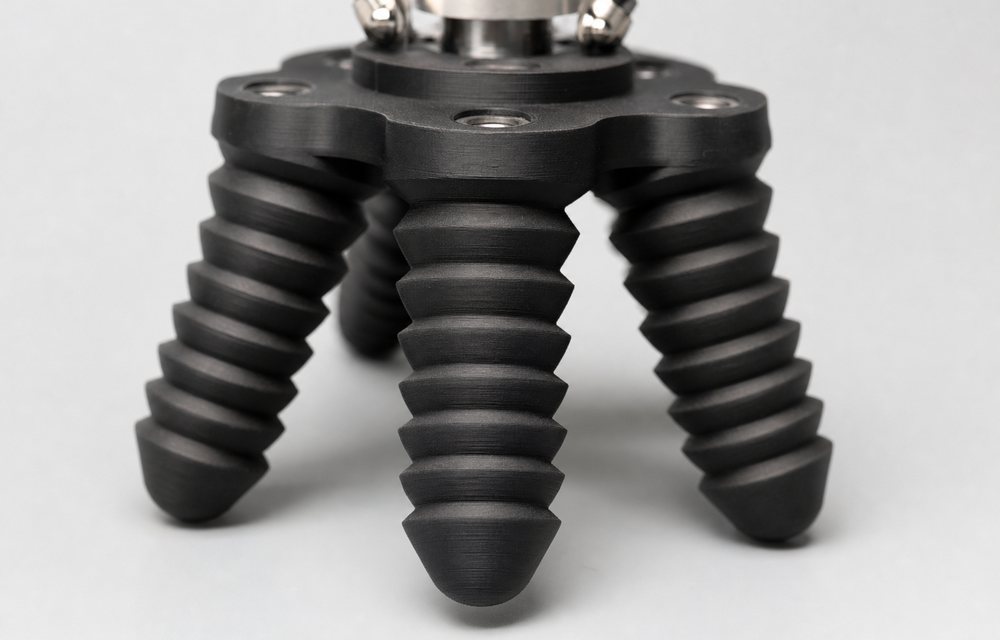
R&D / Prototyping
- Flexible functional prototypes
- Compliant mechanism tests
- Soft gripper fingers
Tensile Strength Across the Range (MPa)
Heat Deflection vs Tensile Strength
Available Materials
When to Use TPU 95A, and When Not To
Use TPU 95A when
- Flexibility and elasticity are the primary design requirement
- Abrasion-resistant surfaces in sliding or wear contact
- Seals, gaskets, or O-rings with custom geometry
- Protective bumpers or cases that absorb impact
- Your machine has a direct drive extruder
Avoid TPU 95A when
- Bowden extruder setups — filament jams in the tube gap
- Continuous use above 55 °C (TPU softens; use silicone instead)
- High-load structural parts — low tensile modulus
- Very fine detail — flexible materials struggle with overhangs
DfAM Tips for TPU 95A
With a flexible material, wall thickness is how you set stiffness. It is a design choice, not a default.

Wall Thickness ≥ 1.2 mm for Stiffness
For structural zones within a TPU part (that should NOT flex), use 4+ perimeters. Thin walls flex everywhere.

Min Hole Diameter: 1.5 mm
TPU can compress and close small holes when assembled. Add 0.2–0.3 mm clearance to any bore that must remain open under compression.

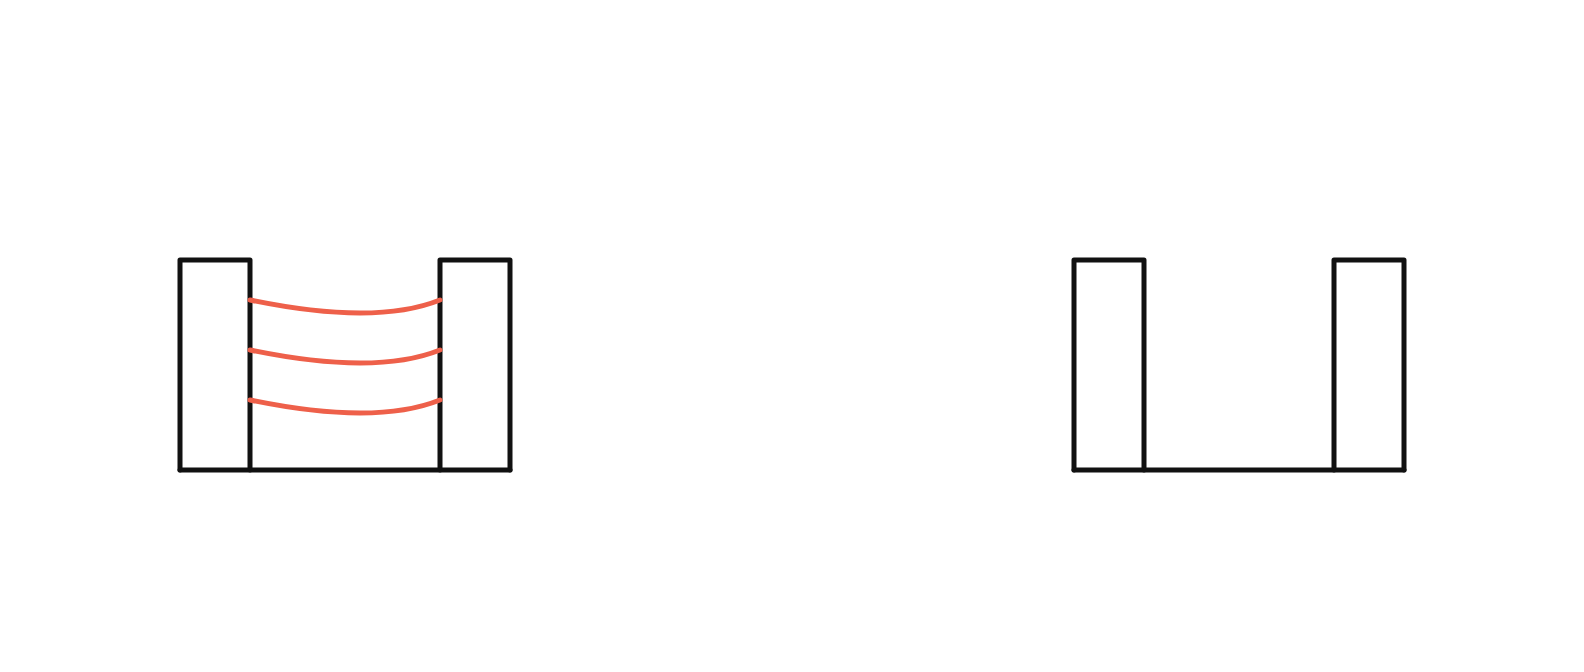
Max Bridge Span: 8 mm
Flexible filament sags quickly on bridges. Keep unsupported spans under 8 mm or add supports. Long overhangs become drooping surfaces.
Disable or Minimise Retraction
Retraction causes TPU to buckle inside the drive gear. Set retraction to ≤ 1 mm at ≤ 25 mm/s. Print speed ≤ 30 mm/s for consistent results.
Printers Compatible with TPU 95A
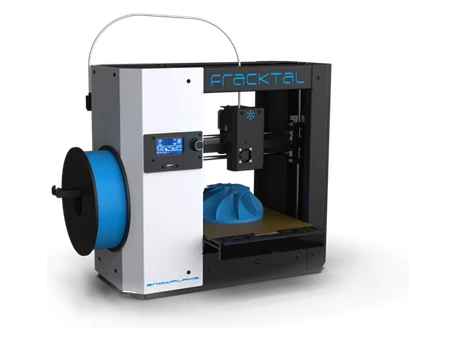
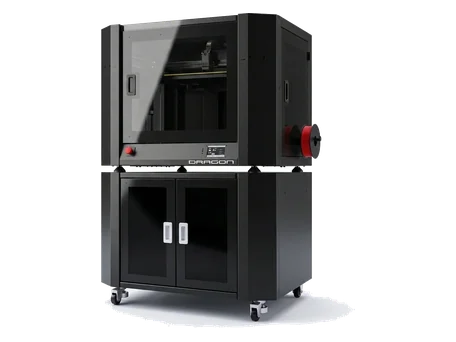
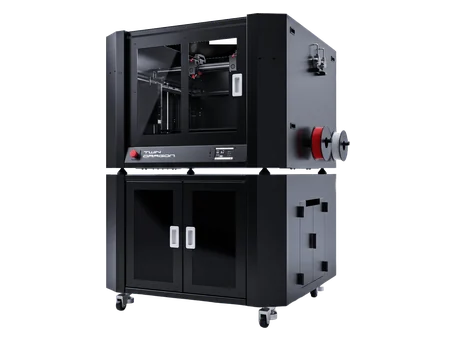
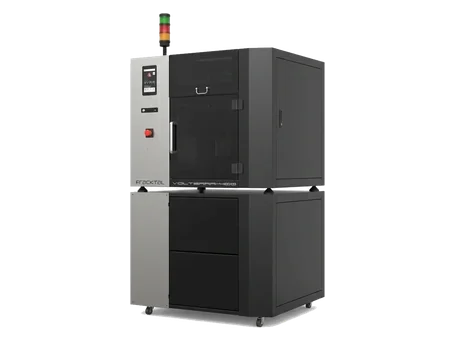
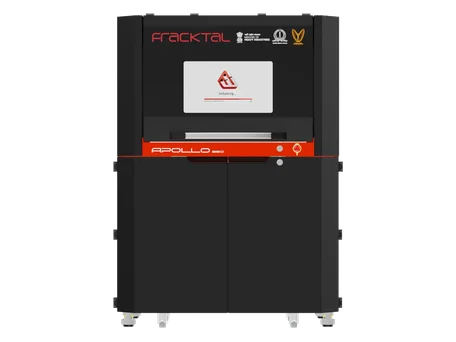
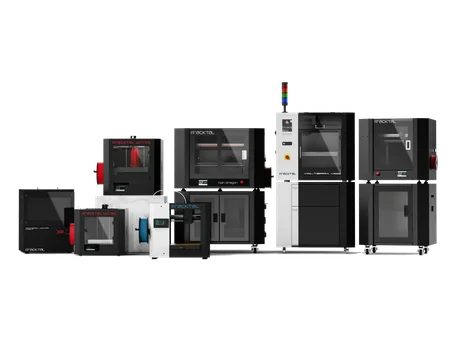
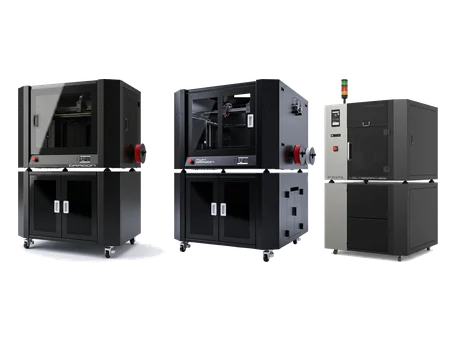
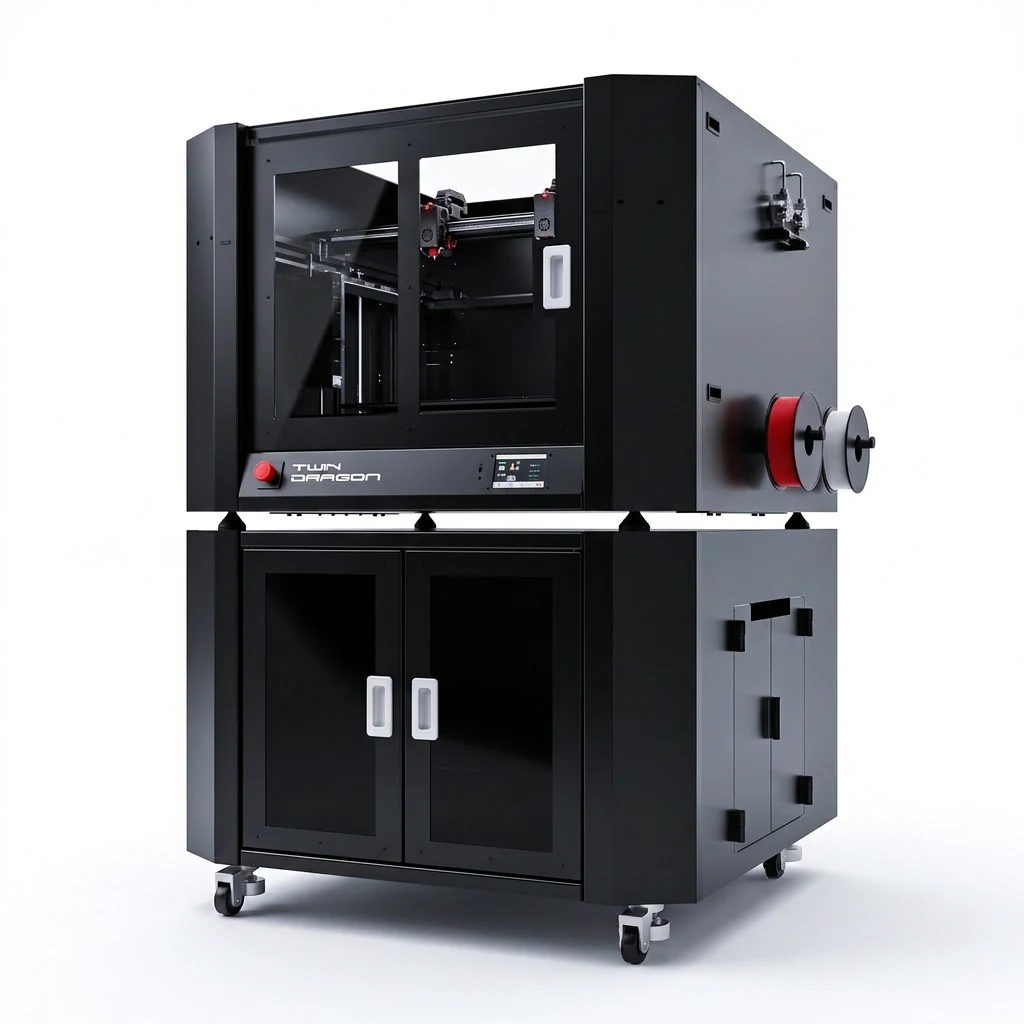
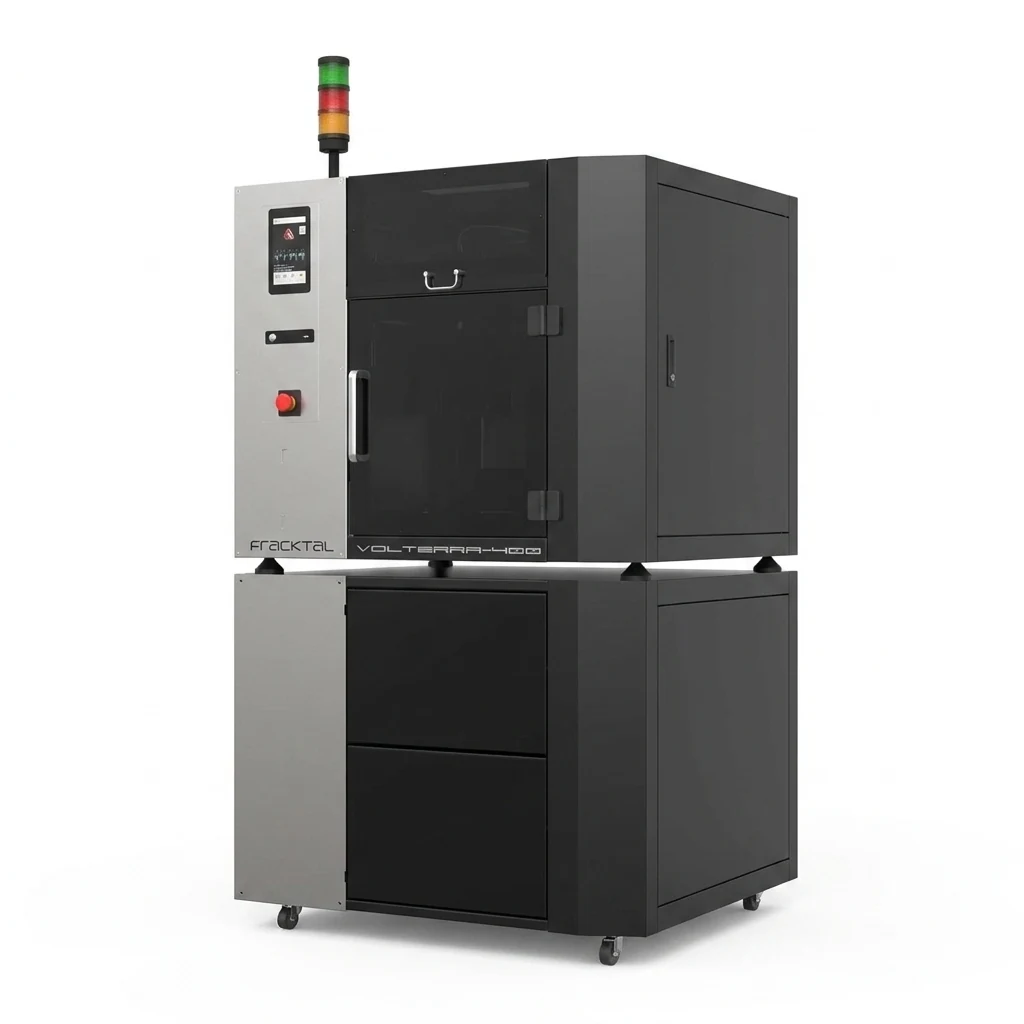
TPU 95A needs a direct drive extruder and moderate temperatures. Dragon, Twin Dragon, Julia, and Volterra all use direct drive, and TPU also runs on the Snowflake desktop printer.


Ready to print in TPU 95A?
Fracktal TPU 95A ships in available in 500 g and 1 kg spools.